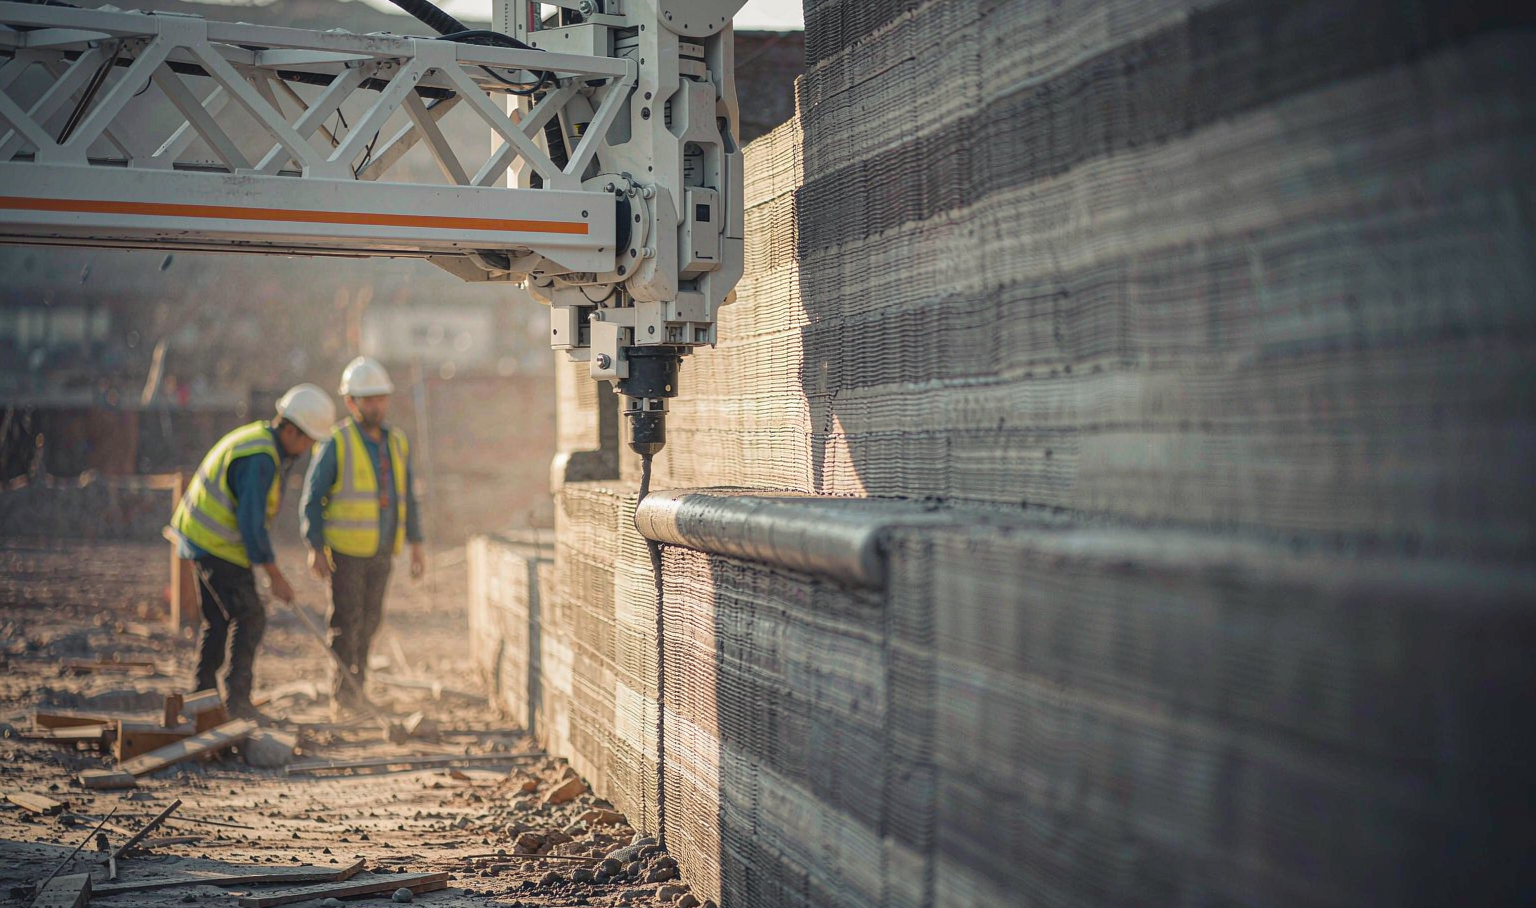
Robotic arms can extrude concrete to print building walls rapidly. However, the load‑bearing capacity and structural‑safety assessment of such walls remain core concerns. Traditional cast‑in‑place concrete follows mature workflows including mix proportion submission, specimen casting, and 28‑day strength reports. For 3D‑Concrete Printing (3DCP), no formwork or vibration is applied, and interlayer interfaces exist. Materials must bear self‑weight immediately upon extrusion. For the same mix proportion, the compressive strength in the Z‑direction (stacking direction) is 20%‑30% lower than in the X‑direction. Flexural and splitting‑tensile strength across layers may drop by 30%‑50%. Thus, strength verification cannot rely solely on cubic compression tests; a complete evidence chain covering materials, components, construction processes and regulatory compliance is required.
1. Why Cast‑in‑Place Concrete Verification Methods Cannot Be Directly Adopted
- Material anisotropy: Printing induces strip orientation, leading to strength discrepancies across directions. According to T/CECS 786‑2020, the printing‑induced strength reduction rate shall not exceed 20%. A 20% reduction may be adopted when test data are unavailable. Design must specify loading directions and reduction coefficients.
- Vulnerable interlayer interfaces: Interlayer time intervals dominate bonding performance. Too short intervals cause crushing of fresh lower layers; excessively long intervals produce cold joints. Wall out‑of‑plane bending and shear capacity are often governed by interfaces rather than the concrete matrix.
- Early‑age instability independent of 28‑day strength: Failures during printing occur at hourly early ages, categorized as plastic collapse and elastic buckling, governed by early green strength and stiffness rather than 28‑day strength. Separate verification is mandatory.
- Amplified defects and size effects: Printing deviations and lap defects reduce effective cross‑sections. Small specimens contain a high proportion of interfaces; their test results cannot be directly extrapolated to full‑scale walls. Full‑scale component tests are indispensable.
2. Four‑Tier Verification Framework and Two Categories of Test Evidence
Four verification tiers cover materials, interfaces, components and projects:
- Material level: Characterize fresh and hardened materials via rheology, tri‑axial compression, elastic modulus, flexure and splitting tension to assess extrudability and buildability.
- Interface level: Conduct direct tension, interlayer splitting and direct shear tests to compare bonding performance under different printing time intervals.
- Component level: Perform full‑scale axial compression, bending, shear and cyclic loading tests on wall panels, columns and beams to reproduce real boundary conditions and failure modes.
- Project level: Implement third‑party assessment, special inspections, on‑site core drilling and load testing to satisfy regulatory compliance.
Destructive Testing (DT) and Non‑Destructive Testing (NDT) shall be applied jointly. Destructive testing determines design parameters, reduction coefficients and failure modes. Non‑destructive testing extends reference benchmarks to practical construction. NDT results without DT calibration carry limited reliability for safety evaluation.
3. Major Domestic and International Testing Standards
International: ISO/ASTM 52939:2023 serves as a process‑qualification framework governing material traceability, printing calibration and process monitoring. It does not replace design approval or strength evaluation. ISO/ASTM 52900 specifies terminology.
United States: ASTM series define test methods; ACI 318 provides structural‑design provisions. ICC‑ES AC509 is the acceptance criterion for 3D‑printed concrete walls. Projects shall obtain an ESR (Evaluation Service Report) for approval, with constraints on interlayer pause duration, special inspection requirements and seismic applicability.
Europe: General Eurocode EN standards are supplemented by national technical guidelines. Project‑specific case‑by‑case approval is adopted, as dedicated complete EN standards for 3D‑printing design and acceptance are not yet available.
China: Association standards T/CECS 786‑2020 and T/CBMF 183‑2022 specify mechanical‑property tests. Industry standard JC/T 2850‑2024 unifies test methods for interfacial bonding strength. JC/T 2914‑2025 and JC/T 2915‑2025 cover shrinkage performance and terminology. Existing concrete standards such as GB/T 50081 and JGJ/T 384 are referenced. Chinese standards distinguish matrix and interface performance and quantify anisotropic strength reduction.
4. Key Tests and Evaluation Criteria
- Tri‑directional compression: Specimens shall be sawn from printed entities and loaded along X/Y/Z directions in compliance with sampling quantity requirements. Outliers shall be eliminated. Design values adopt reduced strength; flat end surfaces and consistent loading rates must be guaranteed.
- Interlayer bonding: Adopt direct tension, splitting and double‑face shear tests. Focus on the ratio of interfacial strength to matrix strength, and establish correlation curves between strength and interlayer time intervals.
- Flexure test: Four‑point bending tests shall be carried out for specimens with and without interlayer interfaces respectively.
- Full‑scale components: Record peak bearing capacity, failure modes and displacement ductility. Ultimate load alone is insufficient for assessment.
- Early‑age performance: Obtain green‑strength rheological curves, conduct build‑to‑failure stacking tests, and cross‑verify instability risks via finite‑element analysis.
- On‑site inspection: Core drilling provides direct physical evidence. Full‑scale load tests may be implemented when necessary to verify consistency between on‑site components and laboratory specimens.
5. Application Boundaries of Non‑Destructive Testing
Common techniques include ultrasonic pulse velocity, rebound test, impact‑echo and ground‑penetrating radar. Acoustic emission and machine‑vision‑based defect identification remain under research. Ultrasonic amplitude attenuation is more sensitive to interfacial defects than longitudinal‑wave velocity. Wave‑velocity readings may produce overly optimistic judgements affected by material anisotropy.
Critical principle: NDT threshold values must be calibrated via destructive tests using identical mix proportions and processes. Uncalibrated NDT results cannot support safety judgements.
6. Regulatory‑Approval Logic
Sufficient test data do not automatically pass plan review. Structural‑safety conclusions shall be issued by qualified entities following local regulatory procedures. In the US, projects follow the alternative‑materials‑and‑methods pathway and obtain ICC‑ES evaluation reports. European projects apply special demonstration based on Eurocodes plus national guidelines. In China, association and industry standards serve as technical foundations, with compliance achieved through local special reviews and expert demonstrations. Regulators require a complete traceable evidence chain covering materials, controlled processes, reproducible tests, clear application scopes and quality‑control measures.
7. Common Misconceptions
- Evaluating component bearing capacity solely by material compressive strength (interfacial tension and shear often dominate failure).
- Equating satisfactory material‑specimen performance with qualified components; ignoring size effects and skipping full‑scale tests.
- Treating ISO/ASTM 52939 process qualification as equivalent to regulatory compliance.
- Determining structural safety exclusively from non‑destructive test results.
- Neglecting the critical influence of interlayer printing intervals on interface bonding, and failing to validate interface equivalence after excessive printing pauses.
Conclusion
Verifying the structural strength of 3D‑printed buildings essentially converts material dispersion into controllable engineering parameters. Enterprises shall complete three key tasks: quantify anisotropy and interfacial reduction coefficients; establish bearing‑capacity benchmarks via full‑scale tests and apply calibrated NDT for on‑site inspection; integrate equipment, materials, processes and quality control into a complete regulator‑accepted evidence chain. Structural‑safety conclusions must be based on measured test data.