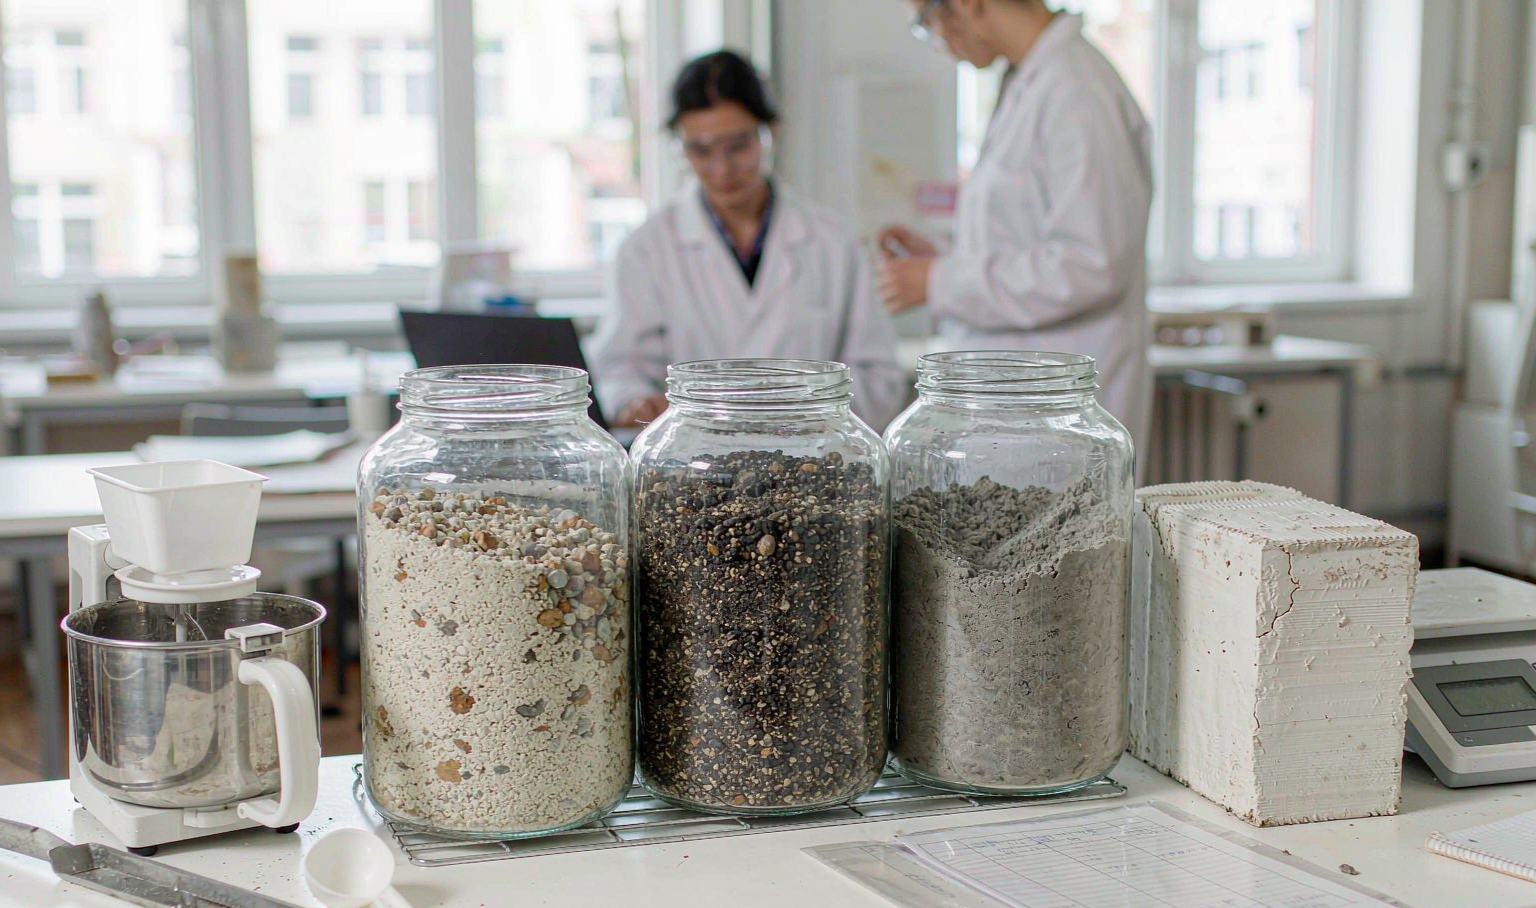
When laying out the formulation for 3D‑printed concrete, aggregates are one of the most unassuming yet highly constrained components. They govern whether the extruded mixture can retain its shape after exiting the nozzle, as well as the performance of hardened walls along the layer‑by‑layer build‑up direction. Recycled materials produced by crushing waste from building demolition fall precisely into this category. This raises concrete questions: can they replace natural aggregates, to what replacement ratio, and who bears responsibility for guaranteeing post‑replacement performance?
Aggregates play a different role in printing formulations compared to conventional concrete
Traditional concrete can accommodate coarse aggregates ranging from 20 mm to 32 mm. A broader particle‑size gradation yields a more stable skeletal framework. 3D‑printing follows a different logic: the mixture must be pumpable and extrudable into continuous filaments. The maximum aggregate particle size is constrained by nozzle geometry; most formulations cap it at 2 mm‑4 mm. Some studies set one‑third of the nozzle diameter as the threshold to prevent nozzle clogging. This means aggregates used in printing formulations mostly fall within the particle‑size range of sand.
Crushing demolition debris readily yields fine‑grade material within exactly this range, whose value is often underestimated. Crushed and screened fines derived from demolished concrete blocks, bricks and old mortar have long been confined to low‑value applications such as road subbases and backfilling. Fine aggregates required for printing formulations have traditionally relied on river sand and manufactured sand. While there is a potential match between supply and demand, two barriers stand in the way: regulatory specifications and processing technologies.
Current specifications mostly grant access to coarse recycled aggregates
The 2021 revision of European Standard EN 206 sets allowable replacement ratios for recycled coarse aggregates, categorized by aggregate type and exposure class. For Type A aggregates containing no less than 95 % combined concrete and unbound aggregate fractions, a 50 % replacement ratio is permitted for the non‑corrosive X0 exposure environment; this drops to 30 % for environments including XC1‑XC4, XF1, XA1 and XD1. Use is prohibited for all remaining exposure classes. For medium‑quality Type B aggregates with a recycled‑concrete fraction of no less than 50 %, the corresponding replacement ratios are 50 % and 20 %. Moreover, Type B aggregates cannot be used in concrete with strength classes higher than C30/37.
An easily overlooked caveat applies here: these provisions target heavy‑weight natural coarse aggregates with particle sizes of at least 4 mm. Fine‑grained printing mortars, whose primary aggregates are smaller than 2‑4 mm, fall outside the scope of this clause. Access for fine‑particle material is provided by another standard: EN 197‑6 published in 2023 allows recycled‑concrete fines to be used as a cement constituent, reclassifying recycled material from aggregate to binder.
This creates a regulatory mismatch: specifications impose ratio caps for coarse aggregates and open a new pathway for ultra‑fine powders. Yet the intermediate particle‑size fraction most needed for printing formulations sits right between these two categories. National annexes adopt divergent approaches, meaning replacement ratios must be verified case‑by‑case according to local project requirements.
Water absorption represents an unavoidable primary constraint
Recycled aggregates retain adhered old mortar on their surfaces, leading to high porosity and substantially greater water absorption compared with natural aggregates. One set of measurements on 3D‑printing mortars recorded river‑sand water absorption at 4.5 %, versus 13.5 % for recycled sand. Another study reported natural fine‑aggregate water absorption of 2 %, compared with 17.6 % for fine aggregates derived from recycled concrete and bricks. Literature reviews cite an upper‑bound water‑absorption value of roughly 14 % for recycled fine aggregates.
Identical mixing water produces vastly different outcomes for the two aggregate types. Natural aggregates barely absorb water, so mixing‑water content directly translates to effective water for hydration. Recycled aggregates absorb part of the mixing water first, causing the effective water‑binder ratio to drift within minutes, which in turn alters yield stress and flowability. 3D‑printing has an extremely narrow processing window: overly fluid mixtures lack inter‑layer support, while overly stiff mixes produce fractured extruded filaments.
Engineering solutions adopt two parallel strategies: supplementary water addition to compensate for aggregate water absorption, together with adjusted admixture dosages corresponding to replacement ratios. In the aforementioned study, 70 % of the absorbed water volume was compensated, while superplasticizer dosage was raised from 1.52 kg/m³ to 2.16 kg/m³ to cover 0‑100 % replacement range. Another study offers finer‑tuned parameters: as recycled fine‑aggregate replacement increases from 0 % to 50 %, water‑retaining agent dosage rises from 1.25 kg/m³ to 1.28 kg/m³, and superplasticizer dosage increases from 0.71 kg/m³ to 0.86 kg/m³.
The practical significance of these figures lies not in their absolute values but in illustrating how recycled aggregates fit into formulations: water absorption is a variable rather than a fixed constant, admixture dosages must track replacement ratios, and one fixed formulation cannot accommodate multiple material batches.
Strength and inter‑layer bonding do not follow a simple monotonic decline
A common concern over incorporating recycled aggregates into printing formulations is strength reduction. Experimental test results are inconsistent, and this inconsistency itself reveals key underlying factors.
One study on recycled‑brick aggregates found that after replacing 64 % of natural aggregates, cubic compressive strength decreased by 25 %, inter‑layer tensile strength fell by 20 %, and compressive strength of printed specimens dropped by 14 % and 20 % respectively under two loading orientations. Another investigation using stone powder to replace natural sand drew range‑based conclusions: both printability and mechanical strength can be maintained at replacement ratios between 20 % and 43 %. Peak compressive strength of 39.9 MPa occurs at 43 % replacement, while peak flexural strength of 10.4 MPa appears at 32 %. Replacement ratios above 54 % are not recommended, as plastic viscosity becomes excessive and post‑shear structural‑recovery capacity deteriorates.
Conversely, some tests report favourable outcomes. In experiments replacing natural sand with recycled fine aggregates at 25 %, 50 % and 100 % substitution rates, 28‑day compressive strength barely changed at low replacement ratios. Full 100 % replacement yielded up to 21 % strength improvement alongside optimal durability performance. The authors attributed this phenomenon to optimised particle‑size distribution and packing efficiency. Further research employed multi‑objective optimisation to adjust mix proportions and printing parameters simultaneously. At a 97 % replacement ratio, buildability improved by 66 %, enabling continuous printing of 6‑10 layers without collapse.
Taken together, these results demonstrate that success does not hinge simply on whether recycled aggregates are added. Instead, it depends on coordinated optimisation of particle‑size gradation, replacement ratio and admixture dosage. It should also be emphasised that nearly all such datasets are obtained from laboratory‑scale specimens measuring only tens of millimetres; these values cannot be directly extrapolated for design of full‑scale building walls.
Real‑world implemented projects
A relatively complete case of 3D‑printed housing using recycled materials is located in Almaty. This 100 m² dwelling is Central Asia’s first 3D‑printed building. Wall printing took five days, and overall construction was completed within two months, engineered to meet seismic‑resistance requirements for magnitude‑7 earthquakes. Its mixture utilises local crushed concrete demolition waste. Mobile crushing equipment and magnetic separators separate concrete from reinforcing steel, after which materials are re‑formulated to satisfy printing specifications. Supported by a productive‑innovation programme funded by the World Bank, the project team is expanding production capacity for neighbouring markets.
Other projects combine recycled aggregates with multiple solid wastes for longer‑term deployment. A two‑storey in‑situ 3D‑printed building with a floor area of 52.8 m² and height of 6 m was delivered in 2023. Its material blend incorporated recycled coarse aggregates, recycled brick powder, recycled sand and tailings sand. The supporting production line can process 500 000‑600 000 tonnes of construction waste annually. Project stakeholders concluded that equipment is not the bottleneck — raw materials are. Months were spent sourcing suitable printing feedstock, given the extremely sensitive time window between mixture extrusion and hardening.
Prerequisites for incorporation into printing formulations
Returning to the core question: incorporating recycled aggregates into 3D‑printing formulations has been repeatedly validated in laboratory settings, with replacement ratios reaching 25 %, 97 % and even 100 %. Nevertheless, stable incorporation into formulations and subsequent deployment in structural applications depends on three preconditions.
First is source‑material sorting. The performance ceiling of recycled aggregates is determined by feedstock quality. Aggregates produced from mixed unsorted demolition waste exhibit highly variable water absorption, which cannot sustain a stable printing processing window. The updated European Protocol for Construction and Demolition Waste Management recommends pre‑demolition audits, so materials can be identified and segregated before entering crushing operations.
Second is reproducible water‑absorption compensation. Formulation design must treat aggregate water absorption as a batch‑dependent input variable rather than a once‑calibrated constant. Site‑side practical challenges also need addressing: recycled‑aggregate moisture content fluctuates with weather, requiring appropriate stockpiling protocols and regular material testing.
Third is the structural function of printed components. Existing proven real‑world applications are largely limited to non‑load‑bearing or low‑load elements: landscape components, envelope walls, municipal furnishings and low‑rise residential walls. Load‑bearing members require far longer validation cycles and must account for direction‑dependent strength disparities inherent to 3D‑printed parts. Multiple tests have recorded 13 %‑20 % performance gaps between specimens loaded parallel versus perpendicular to printing layers; design values must explicitly incorporate this anisotropy.
Finally, consider statistical data. United States Environmental Protection Agency statistics for 2018 report 600 million tons of construction‑and‑demolition waste generated in the United States, more than twice the volume of municipal solid waste. Approximately 313 million tons of this waste was processed into aggregates, representing the single‑largest end use for such debris. The European Union reports construction‑demolition‑waste recycling rates approaching or exceeding the 70 % target. Both datasets point to the same reality: large‑scale pathways already exist for recycled materials to become aggregates, yet the vast majority of output still goes toward road subbases and backfilling. Real improvements in circular‑economy efficiency hinge on diverting more recycled material into high‑value applications previously dominated by virgin raw materials. 3D‑printed components fall squarely within this category. They demand tightly controlled particle‑size gradation, predictable rheological behaviour and traceable material sources. Precisely because of these stringent requirements, once technical hurdles are overcome, recycled materials gain lasting structural‑grade applications that persist beyond individual project lifecycles.